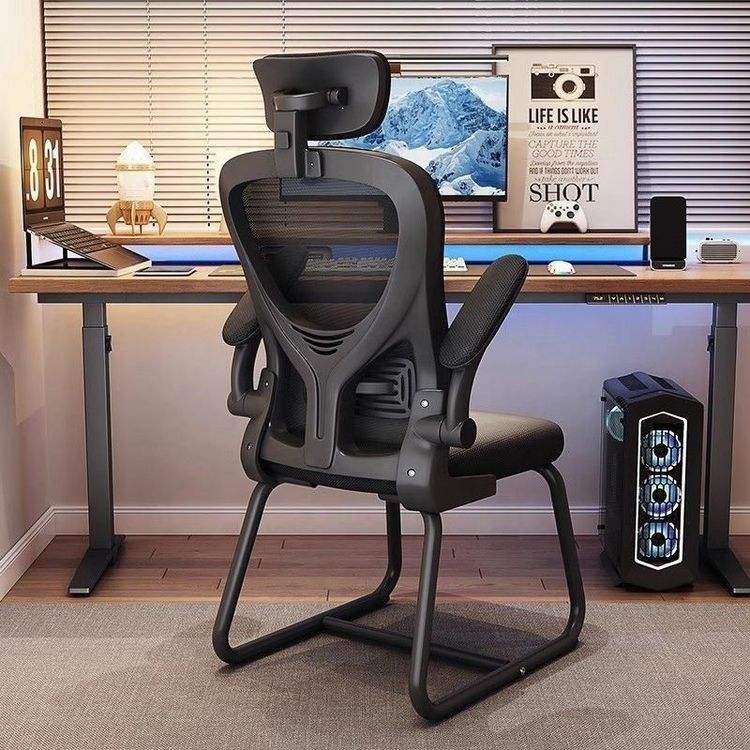
Manufacturing Process of Office Chairs
The manufacturing process of office chairs primarily includes five core stages: raw material selection, component manufacturing, exterior production, assembly and adjustment, and quality inspection.

Raw Material Selection The raw materials for office chairs undergo rigorous testing. Metallic materials (such as steel chair legs and gas lifts) are tested for wall thickness and tensile strength; plastic components (like armrests and backrest shells) are evaluated for impact resistance; and fabrics (mesh, leather, foam) are tested for abrasion resistance, colorfastness, and density rebound rate. For instance, foam density must reach 25-35kg/m³ to ensure support, and leather must pass the Martindale abrasion test (≥50,000 cycles) to guarantee durability.
Component Manufacturing
- Frame Production: Steel tubes are bent into four-cornered, rounded bottom frames using hydraulic presses, and support plates and rods are welded to secure the seat adjustment mechanism. Some high-end seats use mortise-and-tenon joints to connect wooden frames, reducing the risk of metal fatigue.
- Spring Installation: S-shaped steel springs extend from the front to the back of the frame, forming an elastic net, with transverse steel rods fixed by clamps to enhance stability.
- Chair Legs and Gas Lifts: Steel tubes or aluminum alloys are bent and welded into shape, then surface-treated with plastic spraying or electroplating for rust prevention; gas lifts must pass 100,000 lifting cycle tests, with internal high-pressure nitrogen sealing meeting BIFMA standards.
Exterior Production
- Leather Cutting: Plastic templates are used to precisely cut leather, avoiding natural flaws; some processes require bonding leather with rigid foam cushions before cutting.
- Foam Processing: Different density foams are selected based on the part (e.g., 30kg/m³ for seat cushions, 25kg/m³ for backrests), with laser or waterjet cutting ensuring dimensional accuracy.
- Sewing and Assembly: Foam and fabric are sewn together and then fitted onto the frame; particleboard is added to the middle of the backrest for stability, and the base is connected to the support structure via screw holes. Some designs employ 3D cutting techniques to improve fit.
Assembly and Adjustment Components are assembled via assembly lines or robots, with a focus on controlling screw torque (e.g., 8-10N·m for backrest connections) and snap-fit alignment accuracy (error ≤0.2mm). Ergonomic testing simulates sitting pressure distribution for different weights (50-120kg), adjusting the backrest tilt tension (typically 20-30N·m) to optimize support.
Quality Inspection Finished products must pass load-bearing tests (120kg static pressure for 24 hours), stability tests (tilting 15° without tipping), lifting tests (100,000 cycles for gas lifts without leakage), and fabric abrasion tests (Martindale method ≥100,000 cycles). Some factories conduct additional verifications according to BIFMA X5.1 standards, such as armrest pressure resistance (≥100kg) and wheel rolling resistance (≤2N).